 +86 15361670575
 sales@tytech-smt.com


In surface mount technology the reflow oven is the final arbiter of quality. A perfectly deposited solder paste, placed with micrometre accuracy, is still worthless if the thermal profile that follows does not melt the alloy correctly, wet the pads and leads, and cool the assembly without inducing stress. The reflow oven is the machine that turns paste and parts into a permanent electrical and mechanical connection, and it does so by taking a board through a precisely shaped temperature journey — the reflow profile — that every component, every pad, and every gram of paste must survive.
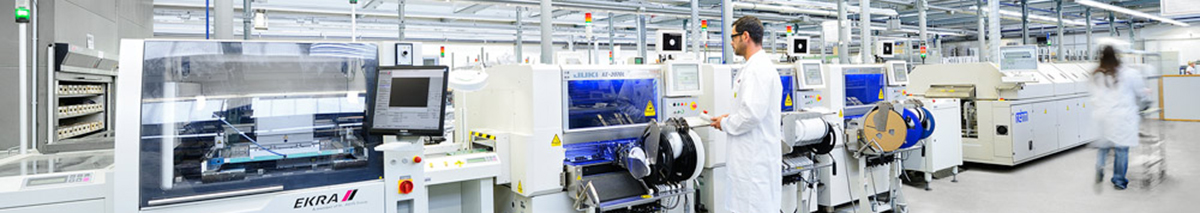
A modern reflow oven is a tunnel furnace, typically divided into preheat, soak, reflow, and cooling zones, through which boards pass on a conveyor at a controlled speed. Heat is delivered and removed by forced convection, with hot air impinging on the top and bottom of the board from independently controlled heater modules. The result is a thermal profile that is repeatable across every board, every shift, and every product changeover — provided the machine, the recipe, and the process are understood.
Why the Reflow Profile Matters More Than Peak Temperature
Most attention in reflow is given to peak temperature, because peak temperature is the number that appears on a datasheet. In reality, the entire shape of the profile governs joint quality, and peak is only one point on that shape. A board that reaches the right peak too quickly will suffer solder balls, component cracking, and voiding; one that reaches it without a proper soak will see uneven melting across the panel as small pads heat before large copper areas.
The standard lead-free profile breaks into four regions. The preheat region ramps the assembly from ambient toward roughly 150 to 170 °C, evaporating the volatile solvents in the paste flux without splattering. The soak or stabilization region holds the board near 170 to 200 °C for a defined time, equalising temperature across the panel and activating the flux chemistry. The reflow region pushes the hottest zones above the alloy liquidus — typically 240 to 260 °C for SAC305 and SAC405 — long enough for wetting to occur, usually 30 to 90 seconds above liquidus. The cooling region then brings the assembly back below the solidus at a controlled rate, defining the grain structure of the joint and locking the components in position.
Each region is a process window. Ramp rate in preheat must stay gentle enough to avoid component shock and paste spattering, commonly below 3 °C per second. Soak duration must balance flux activation against oxidation risk. Time above liquidus must be long enough for wetting but short enough to limit intermetallic growth and tin pest in some alloys. Cooling rate, often overlooked, influences the mechanical strength of the joint: a faster quench refines the grain structure but stresses brittle parts; a slow cool relieves stress but coarsens the joint and weakens it. There is no universal optimum; there is the optimum for a specific board, alloy, and component set.
Forced Convection Versus Infrared Heating
Two heating technologies dominate reflow. Infrared ovens radiate heat onto the board from emitter panels and are inexpensive, compact, and effective for simple boards, but they suffer from colour-dependent absorption and poor thermal uniformity on mixed-mass assemblies. Forced-convection ovens circulate heated air through nozzle arrays onto the board surface and provide far better uniformity, predictable heat transfer, and the ability to profile complex boards reliably. For any production line running lead-free alloys, mixed component sizes, or dense boards, forced convection is the standard choice.
The advantage of convection is its independence from surface emissivity. An infrared oven heats a black plastic connector faster than a shiny copper pad, producing temperature differences across the board that the profile cannot absorb. Convection treats the whole surface as a thermal mass to be heated uniformly, and a well-designed convection module can hold the difference between a large copper ground and an isolated pad to within a few degrees across a 400 mm panel. That uniformity is what makes modern fine-pitch lead-free reflow feasible at production speed.
The compromise is energy. Moving and reheating air consumes more power than radiating heat, and a long forced-convection tunnel with many zones is a significant energy load. Modern machines address this with insulated tunnels, recirculation designs that reuse exhaust heat, and intelligent exhaust management that reduces airflow at idle and light load. Energy management software now claims savings of ten to twenty percent by matching exhaust volume to actual production status rather than running full flow continuously — a meaningful figure when the oven is the largest single consumer on the line.
Zone Architecture and Tunnel Length
A reflow oven is defined as much by the number of its zones as by its temperature range. Each zone is an independently controlled heater module above and below the conveyor, with its own blower, heater element, thermocouple, and PID control loop. The number of zones determines how finely the profile can be shaped; the length of the heated tunnel determines throughput and the achievable ramp rates at production speed.
A compact oven may offer eight heated zones — four top and four bottom — plus a cooling zone, suited to lower-volume or simpler work. A mainstream production platform typically provides ten top and ten bottom heated zones, with a heated length around 3.6 metres and three or more cooling zones, supporting lead-free profiles at conveyor speeds that match high-speed placement lines. Large platforms extend further for heavy boards, dense assemblies, and processes such as vacuum reflow that demand extended time above liquidus.
Cooling zones are not an afterthought. The first cooling zone sets the initial quench rate that defines the as-solidified joint structure, and a machine with three top and three bottom cooling zones can control that rate far more precisely than one with a single passive cooling section. For boards with brittle components, large BGAs, or ceramic parts, the ability to slow the cooling rate independently of the heating zones prevents the cracking that ruins an otherwise good run.
The Conveyor System and Board Handling
The conveyor carries boards through the tunnel on either a mesh belt or a pin chain. Mesh belts suit small-batch and mixed-product work because any board size rides without changeover, but they provide poor bottom-side heating and cannot be used for double-sided boards. Pin chains — edge conveyor systems that grip the board by its edges — are standard in production, supporting the board on rails and leaving the underside exposed to bottom heaters and, where fitted, vacuum modules.
Conveyor width is a primary specification. A typical platform handles boards up to around 350 mm wide, and wider platforms extend to 450 mm or 560 mm for LED panels, server backplanes, and other large-format work. Width changeover is now motorised and recipe-driven, so the line can switch products without manual rail adjustment. Conveyor speed ranges from a few hundred millimetres per minute up to around 1500 mm/min on fast platforms, and the combination of speed and zone temperatures produces the profile that each board experiences.
Board support in the tunnel is a real concern for thin and large boards. A 0.8 mm FR-4 panel spanning 400 mm can sag at reflow temperatures, distorting the print and shifting components. Support wires, centre supports, and wider rail contact patches all mitigate sag, and the choice between them belongs in the specification stage rather than being discovered after the first warped panel. Underside clearance — the height available below the board for components on the second side — determines whether a populated double-sided board can pass without reflowing the first side again, and it should be checked against the tallest bottom-side component at purchase.
Nitrogen Reflow and Oxygen Control
Soldering is a wetting process, and wetting is a competition between flux and oxidation. In air, the flux reduces oxides on pads and leads at the moment of melting, but it must also fight oxide formation throughout the soak and reflow regions. A nitrogen reflow oven floods the tunnel with inert nitrogen, lowering the oxygen level — typically below 1000 parts per million and often below 500 ppm — so that oxidation is suppressed before, during, and after the melt.
The benefits are measurable. Nitrogen extends wetting force, improves the spread of solder on pads, and brightens the joint surface, which simplifies visual and automated optical inspection. It enables the use of low-activity no-clean fluxes, which would struggle to wet in air, and it protects sensitive alloys and surface finishes. For boards with difficult finishes — immersion silver, OSP, or aged tin-lead — nitrogen can be the difference between an acceptable yield and a poor one.
The cost is real. Nitrogen is a consumable, and a large tunnel consumes significant volume. Modern machines reduce consumption through curtain designs that limit gas escape at the entrance and exit, closed-loop oxygen sensing that feeds nitrogen only as needed, and nitrogen recycling where economics justify it. The decision to specify nitrogen is a product decision: high-reliability, fine-pitch, and mixed-finish boards justify it; simple consumer assemblies on gold or tin surfaces often do not. A nitrogen-capable oven can always run in air, but an air-only oven cannot be retrofitted to nitrogen cheaply, so the option is best specified at purchase if the product roadmap includes demanding work.
Vacuum Reflow for Void-Free Joints
Voids — microscopic gas pockets trapped inside a solder joint — are the quiet enemy of power and high-frequency assemblies. A void under a QFN thermal pad reduces thermal transfer and creates a hot spot; voids under a power transistor or a large BGA degrade electrical and thermal performance and can fail qualification outright. The standard reflow profile cannot fully eliminate voids because the gas is trapped during wetting and has nowhere to escape.
A vacuum reflow oven adds a vacuum module in the peak zone. As the joint is molten, the chamber pressure is reduced in stages — commonly five programmable stages — so that dissolved gases and trapped flux volatiles expand and escape the joint before it solidifies. The result is void content below one percent on appropriate geometries, against the several percent typical of conventional reflow. The vacuum stage is programmable independently of the thermal profile, and existing profiles can often be transferred directly, making the technology accessible rather than a process re-invention.
Vacuum reflow is not a universal requirement. It adds cost, complexity, and cycle time, and it is most justified for power modules, RF devices, large-area die attach, and any application where X-ray inspection is a customer requirement. For mainstream consumer assembly it is unnecessary. The platform decision is therefore about the product roadmap: if power electronics, automotive control modules, or advanced packaging are in the plan, a vacuum-capable oven specified early avoids a future line split.
Profile Development and Thermocouple Attachment
A profile is not a guess. It is measured on a real board with real thermocouples attached to the thermally significant points — the largest component, the smallest pad, the ground plane, and any part with a tight temperature window. Thermocouples are attached with high-temperature solder, Kapton tape, or epoxy, each with its own thermal mass and accuracy trade-off, and the board is run through the oven while a data logger records the temperature at each point against time.
The profile is then tuned by adjusting zone setpoints and conveyor speed until every measured point lies within its component-specified window simultaneously. This is harder than it sounds. A large BGA reaches peak temperature ten to twenty seconds after a small chip resistor, and the profile must give the BGA enough time above liquidus without overheating the resistor. The soak region exists precisely to close that gap, equalising temperatures so that all parts reach the reflow region within a narrow band.
Profile development is a one-time-per-product task, but it is also a recurring maintenance task. Heater performance drifts, thermocouples age, fans wear, and the tunnel’s thermal character changes. A profile verified at installation should be re-verified on a schedule — monthly for stable production, more often after maintenance — and any drift that cannot be corrected by setpoint adjustment signals a maintenance need rather than a recipe change. The discipline of profile verification is what separates a stable line from one that produces intermittent field failures.
The Role of Flux and Paste Chemistry
Reflow is not purely a thermal process; it is a chemical process driven by heat. The flux in the solder paste activates during the soak, reducing oxides on the metallisation and the powder itself so that, at liquidus, molten alloy wets the surfaces and forms a metallurgical bond. The activator system — its chemistry, its activation temperature, and its dwell time — must align with the profile, and a mismatch produces either under-activation (poor wetting, cold joints) or over-activation (exhausted flux before melt, voiding, residue).
No-clean fluxes dominate modern production because they leave a benign residue that does not require washing, simplifying the line and reducing cost. Their activity is lower than water-soluble fluxes, which makes profile and atmosphere more critical — another driver for nitrogen on demanding work. Water-soluble fluxes, used where cleaning is required for conformal coating or high-reliability applications, are more active but demand a wash step and tighter process control to prevent corrosion under components.
The paste’s alloy defines the reflow region. SAC305 — tin-silver-copper with 3% silver and 0.5% copper — is the lead-free workhorse, melting around 217 °C and typically reflowed with a peak of 240 to 250 °C. Low-temperature alloys based on bismuth-tin melt near 138 °C and protect heat-sensitive assemblies but have lower fatigue resistance. High-reliability alloys with elevated silver or doped compositions offer better drop and thermal cycling performance at the cost of higher peak temperatures or narrower process windows. The oven does not choose the alloy, but the oven must be specified and profiled to deliver the alloy’s required window repeatably.
Component Temperature Limits and Thermal Shock
Every component on a board has a maximum temperature rating, and the reflow profile must respect the lowest of them. Plastic connectors, electrolytic capacitors, LEDs, and moisture-sensitive devices carry ratings that may sit close to the lead-free reflow peak, leaving little margin. The profile is therefore a compromise: hot enough to wet the most demanding pad, cool enough to survive the most fragile part.
Moisture sensitivity is the silent killer. Plastic-encapsulated components absorb moisture over time, and if they enter the reflow oven without adequate baking, the absorbed water vapourises during the rapid ramp and cracks the package — popcorn cracking — destroying the part invisibly. Moisture-sensitive devices are classified by their floor life, and a controlled dry-pack and bake regime is as much a part of reflow process control as the profile itself. An oven cannot fix a moisture-damaged part; it can only avoid creating one.
Thermal shock is the related failure mode. A ramp rate that is too steep stresses components and metallisation, cracking ceramic capacitors, damaging LEDs, and lifting pads. The preheat ramp is therefore limited, commonly to 1 to 3 °C per second, and the transition between soak and reflow is shaped to avoid a sudden jump. The same discipline applies in reverse in cooling: a quench that is too fast stresses the assembly, while one that is too slow weakens the joint. Both rates are profile parameters, not afterthoughts.
Defects, Root Causes and Profile Solutions
Reflow defects are rarely random. Each has a characteristic cause and a characteristic fix, and an engineer who reads defects correctly can often solve a problem from a single failed board.
Solder balls appear as tiny spheres beside pads and leads, and they typically indicate a ramp rate that is too steep in preheat, causing the paste to slump and spatter before the solvent has fully evaporated. Cold or dull joints indicate insufficient peak temperature or insufficient time above liquidus, leaving the alloy incompletely melted; the fix is a higher peak or a slower conveyor. Voids in BGA and QFN joints indicate trapped gas, addressed by extending the soak to let volatiles escape, by switching to nitrogen, or in extreme cases by vacuum reflow. Tombstoning — a passive component standing on one end — indicates uneven heating between the two pads, often fixed by adjusting the soak or by redesigning the pad geometry. Bridging between fine-pitch leads indicates too much paste or insufficient wetting, the latter often a flux-activity or atmosphere problem.
The discipline is to read the defect, form a hypothesis, and verify it on a single profile run with thermocouples on the affected area. Shotgun adjustments — raising peak temperature to fix a wetting problem, slowing the conveyor to fix a solder ball — often introduce new defects while masking the original. The oven is a precision instrument; treating it as one is the difference between a stable process and a recurring crisis.
Profile Measurement and Verification
A profile is only as good as its last verification. The industry standard is a datalogger that travels through the oven on the conveyor, recording temperature from multiple thermocouples against time, and software that overlays the measured profile against the recipe window and the component limits. The same board, instrumented at the same points, run on the same recipe, should produce the same profile within a degree or two week after week.
Verification frequency depends on risk. For automotive, medical, and aerospace production, a profile check before every product run is common, and a continuous check via a sacrificial board or a fixed reference panel is becoming standard. For consumer work, weekly or monthly verification may suffice, but the principle is the same: the profile drifts, and unmeasured drift becomes field failure. Modern ovens support this with pass-through data ports and recipe-linked thermocouple positions, so verification is a defined procedure rather than an ad-hoc event.
The KPI is the temperature delta across the board at peak — the difference between the hottest and coldest measured points. A delta of five degrees is excellent; ten is acceptable; fifteen is a warning that the board cannot be profiled within all component windows simultaneously and that the design, the component mix, or the oven needs attention. Reducing that delta, through soak tuning, conveyor speed, or zone setpoints, is the central craft of profile engineering.
Oxygen Monitoring and Atmosphere Integrity
In a nitrogen oven, the atmosphere is a process parameter. The oxygen level in the peak zone determines how aggressively oxides form on the molten solder, and a stable low-oxygen atmosphere is what delivers the wetting and spread that justify the nitrogen cost. Oxygen is measured by a sensor in the tunnel, typically at the peak zone, and the reading is displayed and logged alongside the thermal profile.
Atmosphere integrity depends on the tunnel’s physical design. Curtains at the entrance and exit limit nitrogen escape; internal baffles direct flow; the exhaust balance pulls flux volatiles out without disturbing the inert blanket. A machine with poor atmosphere integrity consumes more nitrogen for the same oxygen level, and the cost difference compounds over years. When specifying a nitrogen oven, the consumables per board — nitrogen volume, oxygen achieved, and the stability of that oxygen under load changes — matter as much as the heated zone count.
Drift in the oxygen reading is a maintenance signal. A sensor that drifts may report a safe level while the actual atmosphere has degraded, and periodic calibration or sensor replacement is part of standard maintenance. The same applies to the heater thermocouples, the conveyor speed encoder, and the blower motors: a stable profile and a stable atmosphere depend on instruments that read true, and instruments that read true depend on a calibration schedule.
Energy, Exhaust and the Factory Environment
A reflow oven is the largest single thermal load on most SMT lines, and its exhaust is the largest single contribution to the factory’s heat and fume load. The exhaust pulls flux volatiles, particulates, and heated air out of the tunnel, and it must be balanced: too little exhaust lets flux condense in the machine and the factory, coating surfaces and degrading heaters; too much exhaust wastes heat and nitrogen and pulls the profile cold.
Modern machines manage exhaust intelligently. Variable-speed exhaust fans adjust to production status, running at full flow during peak production and reduced flow at idle or light load, saving both energy and nitrogen. Flux filtration — condensation traps, heat exchangers, and in some cases catalytic oxidisers — protects both the machine and the factory air quality, and the filter maintenance interval is a real operating cost that belongs in the total-cost-of-ownership calculation.
The factory environment affects the oven in return. Ambient temperature swings change the tunnel’s thermal baseline; a factory that runs cold at night and warm at day will see profile drift unless the oven’s controls compensate. Compressed air quality, electrical supply stability, and floor vibration all influence long-term stability, and a well-sited oven in a controlled environment outperforms an identical oven in a draughty corner. Specification is not only about the machine; it is about the machine in its setting.
Throughput, Line Balance and the Oven as Bottleneck
The oven is the slowest fixed-cycle machine on most SMT lines, because every board must traverse the full tunnel length at a speed that produces the profile. Unlike a printer or a mounter, the oven cannot be sped up by adding heads or rails; it can only be lengthened or paralleled. Throughput is therefore conveyor speed times board pitch, and the profile sets the conveyor speed.
Line balance requires the oven’s throughput to match the mounter’s output. If the mounter places a board every twelve seconds and the oven requires a sixteen-second dwell, the oven is the bottleneck and the line runs at sixteen seconds regardless of the mounter’s capability. The common solutions are a longer tunnel with more zones — allowing a higher conveyor speed for the same profile — or a dual-lane configuration that runs two boards in parallel. Both add capital cost, and the choice depends on the product mix and the projected volume.
Changeover affects the oven differently from other machines. A recipe change is fast — zone setpoints and conveyor speed load in seconds — but the thermal stabilisation after a change is not. A large tunnel takes minutes to settle to a new profile after a setpoint change, and a line that changes products frequently loses oven capacity to stabilisation time. Recipe groups that share similar profiles, and scheduling that minimises thermal transitions, are practical responses; a machine with fast-stabilising heaters and good insulation reduces the loss further.
Integration, Traceability and Industry 4.0
The oven is a data source as much as a heat source. Every board that passes carries a thermal record — the profile it experienced, the zone setpoints, the oxygen level, the conveyor speed, the timestamp — and that record is increasingly a customer requirement. Traceability for automotive (IATF 16949), medical (ISO 13485), and aerospace work demands that each assembly’s thermal history be retrievable, and the oven is the machine that produces it.
Modern ovens expose this data through standard interfaces. IPC-CFX and IPC-HERMES-9852 have replaced the bespoke protocols of earlier generations, allowing the oven to publish board-level events, profile data, and machine status to a manufacturing execution system without custom integration. The oven reports not only what it did but how it did it: heater health, blower status, oxygen trend, exhaust balance, and maintenance alerts, all available to factory software that can correlate them with downstream yield data.
Beyond reporting, analytics are entering reflow. Models trained on historical profile and yield data can predict when a heater is drifting before it affects the profile, recommend setpoint adjustments as a thermocouple ages, and flag boards whose measured profile deviated from the recipe even before inspection. None of this replaces process engineering; it extends it, turning the oven from a black box into an instrument whose behaviour is visible and whose drift is predictable.
Cleaning, Curing and Multi-Process Use
The reflow oven’s thermal capability is not limited to soldering. The same controlled tunnel serves curing applications — epoxy and adhesive curing for underfill and encapsulation, drying of solder paste and conductive inks, and baking of moisture-sensitive components before reflow. A machine specified for soldering can often support these processes with a different profile, and multi-process use improves capital utilisation in lower-volume factories.
Infrared curing ovens occupy a related niche. Compact and energy-efficient, they suit fast curing of adhesives, inks, and pastes where the precise multi-zone control of a full convection reflow oven is unnecessary. For high-speed, high-reliability electronics manufacturing they complement rather than replace convection reflow, handling curing and drying steps that do not require the full profile shape. The choice between a dedicated curing oven and a multi-purpose reflow oven depends on volume, product variety, and the value of avoiding process cross-contamination.
The risk in multi-process use is contamination. Flux residues from soldering, adhesive volatiles from curing, and ink solvents all deposit in the tunnel over time, and running different processes in the same tunnel without cleaning risks cross-contamination that shows up as defects. Dedicated tunnels for distinct chemistries are the clean solution; shared tunnels demand a documented cleaning regime and an acceptance of the residual risk.
Reliability, Maintenance and Total Cost of Ownership
A reflow oven is a long-life asset, and its cost is dominated not by the purchase price but by the operating cost over its life. Energy is the largest line — a ten-zone convection oven draws significant power whenever it is at temperature, and an oven left hot overnight consumes power for no production. Nitrogen, where used, is the second-largest consumable. Flux filters, conveyor chains, heater elements, and blower bearings complete the consumable list.
Maintenance is the lever that controls both cost and quality. Daily tasks include cleaning the entrance and exit curtains, inspecting the conveyor chain, and checking the exhaust balance. Weekly tasks cover flux filter inspection and tunnel interior cleaning. Periodic tasks include heater calibration, thermocouple verification, oxygen sensor calibration, and blower inspection. A machine with a documented maintenance schedule runs stable for years; one without drifts, and drift becomes scrap and field failure.
Total cost of ownership should be modelled before purchase. The relevant figures are energy per board at the target profile, nitrogen per board if applicable, consumable cost per thousand boards, mean time between interventions, and the local support and spares availability that determines downtime length. An oven that is cheaper to buy and more expensive to run is not the cheaper oven, and an oven with poor local support is a production risk regardless of its specification.
Selecting the Right Reflow Oven
The selection process begins with the product. Board size range, component mix, alloy, throughput target, and the reliability class of the end product define the minimum specification. A platform handling boards up to 350 mm with SAC305 and a moderate throughput target is well served by a ten-zone convection oven; a line running 560 mm LED panels, vacuum joints, or automotive power modules demands a larger, nitrogen-capable, and possibly vacuum-equipped platform.
The specification checklist is straightforward: heated zone count and length, cooling zone count, maximum board width and weight, conveyor speed range, maximum temperature, nitrogen option and achievable oxygen level, vacuum option, exhaust management, data interface support, and the software that ties them together. Each should be quoted with a measurable figure, not a marketing adjective.
Service closes the specification. Heater and blower availability, thermocouple and sensor lead times, local technical support, training, and the cost of a five-year consumable and maintenance plan determine whether a well-specified oven becomes a stable production asset or a recurring problem. The oven is a fifteen-year decision; it deserves a fifteen-year evaluation.
The Future of Reflow Soldering
Three currents are visible in the evolution of reflow. The first is the continued push toward finer pitch and denser assembly, which demands tighter profile control, better atmosphere integrity, and finer zone resolution. The second is the rise of power electronics and advanced packaging, which drives vacuum reflow, flux management, and profile shapes that conventional tunnels struggle to deliver. The third is intelligence: ovens that adjust their own profiles from in-line measurement, predict heater failure, and report process health rather than just process data.
Sustainability is the fourth, less visible current. Energy and nitrogen consumption, flux emission treatment, and the avoidance of scrap through stable processing are all under scrutiny as factories report environmental performance alongside financial performance. The oven, as the line’s largest energy consumer, is the natural focus of efficiency programmes, and the machines that win in the coming decade will be those that deliver a stable profile with the least energy, the least nitrogen, and the least waste.
Through all of this, the fundamental physics is unchanged. Reflow soldering is the controlled melting and solidification of an alloy to form a permanent joint, and the reflow oven is the instrument that performs that control. The technology that surrounds the physics — the zones, the convection, the nitrogen, the vacuum, the data — is what makes the physics reliable at production scale. Manufacturers who understand both the physics and the technology are the ones whose lines produce joints that survive thermal cycling, mechanical shock, and years of field service — and in surface mount technology, that is what a reflow oven is for.
Practical Takeaway
Specifying a reflow oven is a decision about the thermal integrity of every assembly the line will produce. The cost of the oven appears on a quotation. The cost of an unstable thermal profile appears later — in voids, in cracked capacitors, in dull joints that fail inspection, and in field returns that trace back to a profile that drifted without anyone noticing.
The specifications that matter are the ones quoted with process meaning: zone count and heated length, cooling control, conveyor width and speed, nitrogen and achievable oxygen, vacuum capability, exhaust management, and data interface support. The features that matter are the ones that hold the profile stable across shifts and product changes: precise PID zone control, well-insulated tunnels, intelligent exhaust, recipe-driven changeover, and profile verification supported by the machine.
Above all, reflow is a system that links paste, flux, components, atmosphere, and thermal history into a single outcome. A world-class oven cannot rescue a profile developed without thermocouples, and a perfect profile cannot compensate for moisture-damaged components or an exhausted flux. Manufacturers who treat reflow as a measured, documented, continuously verified process are the ones whose lines produce joints that pass inspection today and survive the field tomorrow — and in electronics manufacturing, that is what reliable solder joints are actually for.
Post time: Nov-10-2026


